English
 日本語
 Français
 Español
 عربى
 italiano
Industry News
 Sep 21, 2026
 Posted by Administrator
Consumer Packaging Design: Structure, Cost, and Sourcing Decisions for Brands
A bakery chain signs off on a windowed cake box in March. By the time 40,000 units reach the chilled aisle in July, the film window has fogged, the die-cut corners have cracked on two pallets, and the kraft tone no longer matches the in-store display it was approved against. Nothing went wrong with the illustration. Everything went wrong with the specification.
Consumer packaging design is a manufacturing decision before it is a graphic one. Structure decides what survives a pallet stack, material grade decides how long the product stays sellable, and the print method decides whether the colour approved in a PDF survives contact with a press. Brands that treat these as production details after artwork sign-off usually pay for the same change twice: once in a reprint, once in returns.
Conclusion first: lock four variables in this sequence - structure, material and barrier, print and finish, then graphics and copy. Reversing that order is the single most expensive habit in consumer packaging design, because every downstream change re-opens the dieline, the tooling, and the print plates at the same time.
The guidance below is written for buyers, brand managers, and product developers sourcing printed paper packaging in runs of roughly 1,000 to 500,000 units, where a 2 mm dieline error becomes a four-figure loss and a 0.5 mm tolerance slip becomes a filling-line stoppage.
Content
- 1 The Four Decisions That Shape Consumer Packaging Design
- 2 Comparing Common Formats: Cost, Tooling, and Fit
- 3 The Hidden Metrics Most Buyers Never Track
- 4 Where Consumer Packaging Demand Actually Sits
- 5 Cost, Tooling, and ROI: A Practical Selection Path
- 6 Compliance, Maintenance, and Storage Discipline
- 7 What to Ask a Manufacturing Partner
The Four Decisions That Shape Consumer Packaging Design
Most design briefs arrive at a factory as a finished illustration plus a rough dimension. That is a brief for a poster, not a package. A production-ready brief answers four questions in order, and each answer constrains the next one.
1. Structure and dieline
Board thickness drives crease geometry. A 350 gsm carton creases cleanly at 0.5 mm depth; a 1,200 micron rigid wrap does not. Die-cut tolerances of plus or minus 0.5 mm are normal, glued seam tolerances of plus or minus 1 mm are normal, and anything tighter than that belongs on a filling line specification, not a wish list.
2. Material and barrier
Uncoated kraft breathes, coated white card resists grease, and metallised or aluminium-laminated film blocks oxygen and moisture. For roasted coffee, an oxygen transmission rate under 5 cc per square metre per day at standard conditions is the practical target, which is why a one-way degassing valve plus a high-barrier laminate is the standard construction rather than a premium upgrade.
3. Print and finish
Offset lithography holds a colour difference of 3 or less on the CIE scale across a long run; flexographic printing is faster and cheaper at volume but harder to hold below 5 on dense solids. Soft-touch lamination hides scuffs, matte lamination shows fingerprints, and heavy foil stamping can break the fibre structure enough to crack at a crease.
4. Graphics, copy, and compliance
Leave a quiet zone of at least 2 mm around any barcode edge, keep allergen and net-weight text at a legibility that survives a 30 percent shrink on shelf, and confirm that the front panel copy matches the destination market before the plates are burned. Compliance text changed after plating is a full reprint, not an edit.
Where all four decisions are made at the same time, the brief produces a package that fills, ships, and sells. Where structure is treated as a checkbox, the design brief quietly becomes a reprint order.
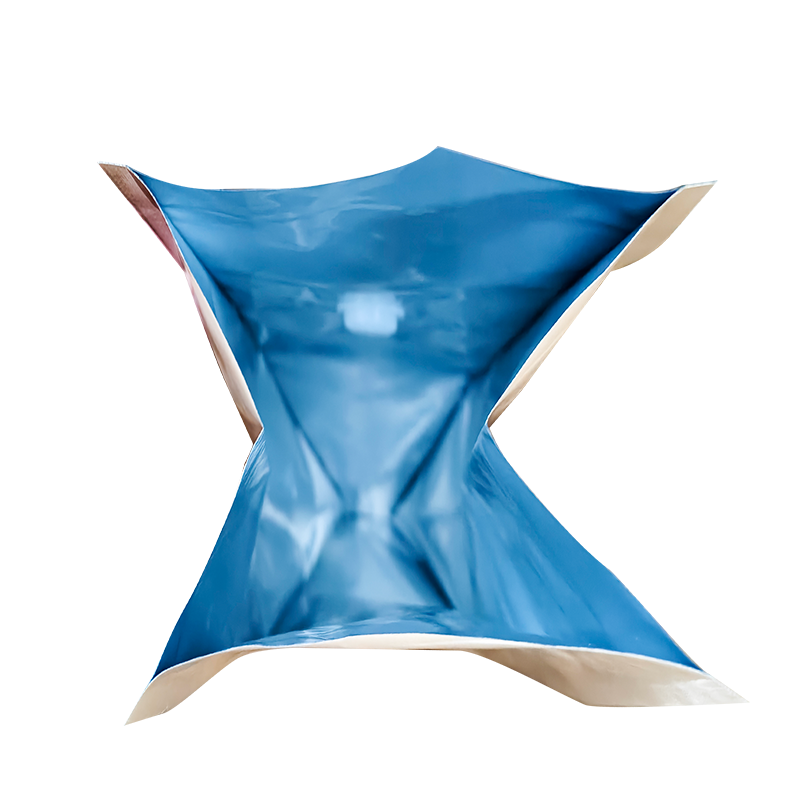 Coffee flexible packaging bag (with vent valve/easy tear opening)Coffee Flexible Packaging Bag (with Degassing Valve / Tear Notch) is constructed from multi-layer high-barrier laminates (typically PET/AL/PE or PET/VMPET/PE), offerin...View Product →
Comparing Common Formats: Cost, Tooling, and Fit
Format choice is usually framed as an aesthetic question. In practice it is a tooling question with a cost-per-unit answer attached to it, and the numbers move faster than most brand teams expect between a 5,000-unit trial and a 50,000-unit reorder.
Read the tooling column as a risk column. A $2,500 rigid-box die spread across 5,000 units adds $0.50 per unit; spread across 50,000 units it adds $0.05. Below roughly 5,000 units, folding cartons, paper bags, and pouches almost always win on landed cost. They lose on perceived value, which is why gifting, skincare, and premium confectionery still default to rigid construction and absorb the tooling.
Low-tooling formats have their own ceiling. Recyclable kraft takeaway bags and semi-rigid food boxes keep plate costs under $900, but they cannot deliver the magnetic closure or the nested tray that a premium gift set depends on. Match the format to the price point, not to the mood board.
 Rigid compartmentalized cake paper tray (for cupcakes, muffins & mini cakes)A high-functionality inner support solution essential for small-format cakes—delivering shape retention, hygiene, visual polish, and cost efficiency in one integrated ...View Product →
The Hidden Metrics Most Buyers Never Track
Field failures rarely trace back to the illustration. In first-run production data across a typical twelve-month cycle, five root causes account for almost every packaging complaint that survives quality control.
Barrier shortfall and transit compression together account for almost half of all failures, yet neither appears on most packaging briefs. Barrier failure shows up as stale product or a sachet that has absorbed ambient moisture before the sell-by date. Transit compression shows up as crushed corners after a stacking test that was never run.
Two checks close most of that gap. First, run a distribution simulation to a recognised protocol such as ISTA 3A or ASTM D4169 before tooling is cut, using the real filled weight and the real pallet height. Second, verify moisture and oxygen performance with a shelf-life trial at accelerated conditions rather than accepting a film supplier's data sheet as proof for your specific fill.
Where Consumer Packaging Demand Actually Sits
Category mix matters more than most buyers assume, because it determines which structures a factory runs every day and which ones carry a learning curve. The distribution below reflects the enquiry pattern across custom paper packaging projects, and it shapes lead times as much as it shapes price.
- Food and beverage: 38 percent
- Beauty and personal care: 24 percent
- Gifts and festive runs: 17 percent
- Apparel: 12 percent
- Home textile: 9 percent
Food and beverage volume keeps kraft, grease-resistant, and barrier-film capacity busy year round. Beauty and skincare demand concentrates in rigid lid-and-base and drawer constructions, where unit prices are four to six times higher and quality expectations follow. Festive work is the most seasonal block: capacity between September and December tightens first, so gift projects that confirm tooling in the first half of the year routinely save both money and schedule risk.
Cost, Tooling, and ROI: A Practical Selection Path
A packaging project runs through five gates. Skipping any one of them moves the cost downstream, where it multiplies.
1. Brief and dieline (2-3 days)
Confirm format, board grade, dimensions, filled weight, stacking height, and shipping route. Vague stacking height is the most common cause of a late structural change.
2. Structural sample (3-5 days)
Cut a white sample and run it through your actual filling or packing process. Fit problems are cheap to fix here and expensive to fix after tooling.
3. Print proof (3-7 days)
Approve a colour drawdown on the final substrate with the final finish. Lamination shifts perception, so approving on uncoated stock is a known trap.
4. Production (12-18 days)
Approve the first article off the line, then audit inline. Rigid boxes run slower than folding cartons, and hot-stamped or windowed work slower again.
5. Inbound QC (2-3 days)
Sample against an agreed acceptance limit, verify packed carton counts, and file the batch-level material declarations alongside the shipment.
The ROI case is easier to build than most teams expect. If a redesigned insert costs $1,200 in new tooling and cuts in-transit damage from 3.5 percent to 1.2 percent, a 20,000-unit order at $4.00 landed value avoids roughly 460 damaged units worth about $1,840. The tooling pays for itself inside the first run, and every reorder after that carries the saving with no additional cost.
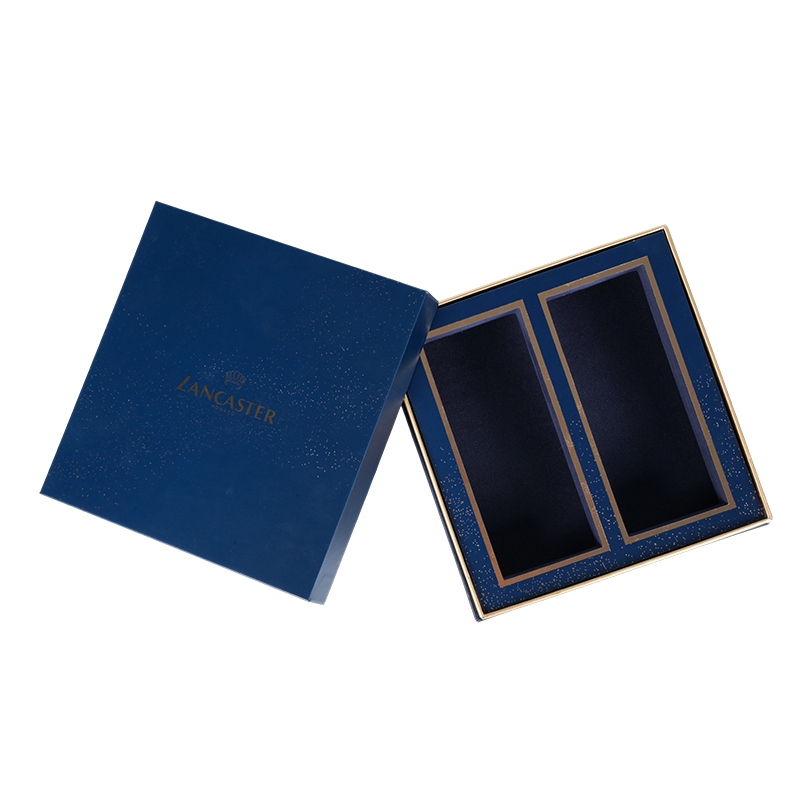 LANCASTER MONACO Luxurious Deep Blue Matte & Gold-Stamped Two-Piece Gift BoxThe LANCASTER MONACO luxury gift box is meticulously crafted using the classic "lid-and-base" mounting technique. Constructed upon a high-density greyboard core, it is...View Product →
Compliance, Maintenance, and Storage Discipline
Compliance failures do not announce themselves on the shelf. They surface in customs, in a retailer audit, or in a recall notice months after the run has shipped.
- Confirm food-contact status for the destination market: EU 10/2011, US FDA 21 CFR 176.170 for paper and board, and GB 4806.8 for food-contact paper in China.
- Specify low-migration inks and coatings where direct or near-direct food contact is possible, and avoid mineral-oil-based offset inks on primary food packaging.
- Treat migration testing and declarations as batch-level documents, not project-level paperwork, so an audit can be answered with the shipment in question.
- Store finished packaging between 15 and 25 degrees Celsius at 45 to 60 percent relative humidity. Laminated board in a damp warehouse warps within weeks, and warped board jams filling lines.
- Review recyclability honestly: film windows, foil stamping, and heavy lamination reduce paper recovery, so mono-material alternatives are worth quoting at the design stage rather than after.
Buyers tracking regulatory movement should watch the third-party research on food-contact packaging safety, which covers migration findings and material substitution trends that often reach procurement requirements a year later.
What to Ask a Manufacturing Partner
Most quality problems in consumer packaging design trace back to handoffs between a designer, a printer, and a box-maker. Fewer suppliers in the chain means fewer places for a 0.5 mm tolerance to disappear.
- Ask whether printing, die-cutting, foil stamping, lamination, and box-making happen under one roof or across four vendors.
- Ask for the sample lead time separately from the production lead time, and confirm which one applies to a reorder.
- Ask for the quality management certification and the acceptance sampling plan used on the final inspection.
- Ask how material declarations for food-contact or cosmetic packaging are issued, and whether they are batch-linked.
- Ask for two recent export references in your own category, then check their delivery timelines rather than their compliments.
A packaging programme that starts with structure, holds tolerances through tooling, and closes with batch-level documentation will not eliminate every surprise in a supply chain. It will move the surprises to the drawing board, where they cost a conversation instead of a container.
Product Categories
Mainly engaged in various types of packaging boxes made of different materials and various paper products.

-
Email
[email protected]Phone Number
+86-15300896380 -
Address
No. 58 Hongmudan Road, Songjiang District, Shanghai, China -
Quick Links
Home About Us Service Industries News Contact -
Products
Food Packaging Cosmetic Packaging Gift Wrapping Apparel Packaging Home Textile Packaging Other Packaging Paper Packaging Boxes -
feel free to contact us